


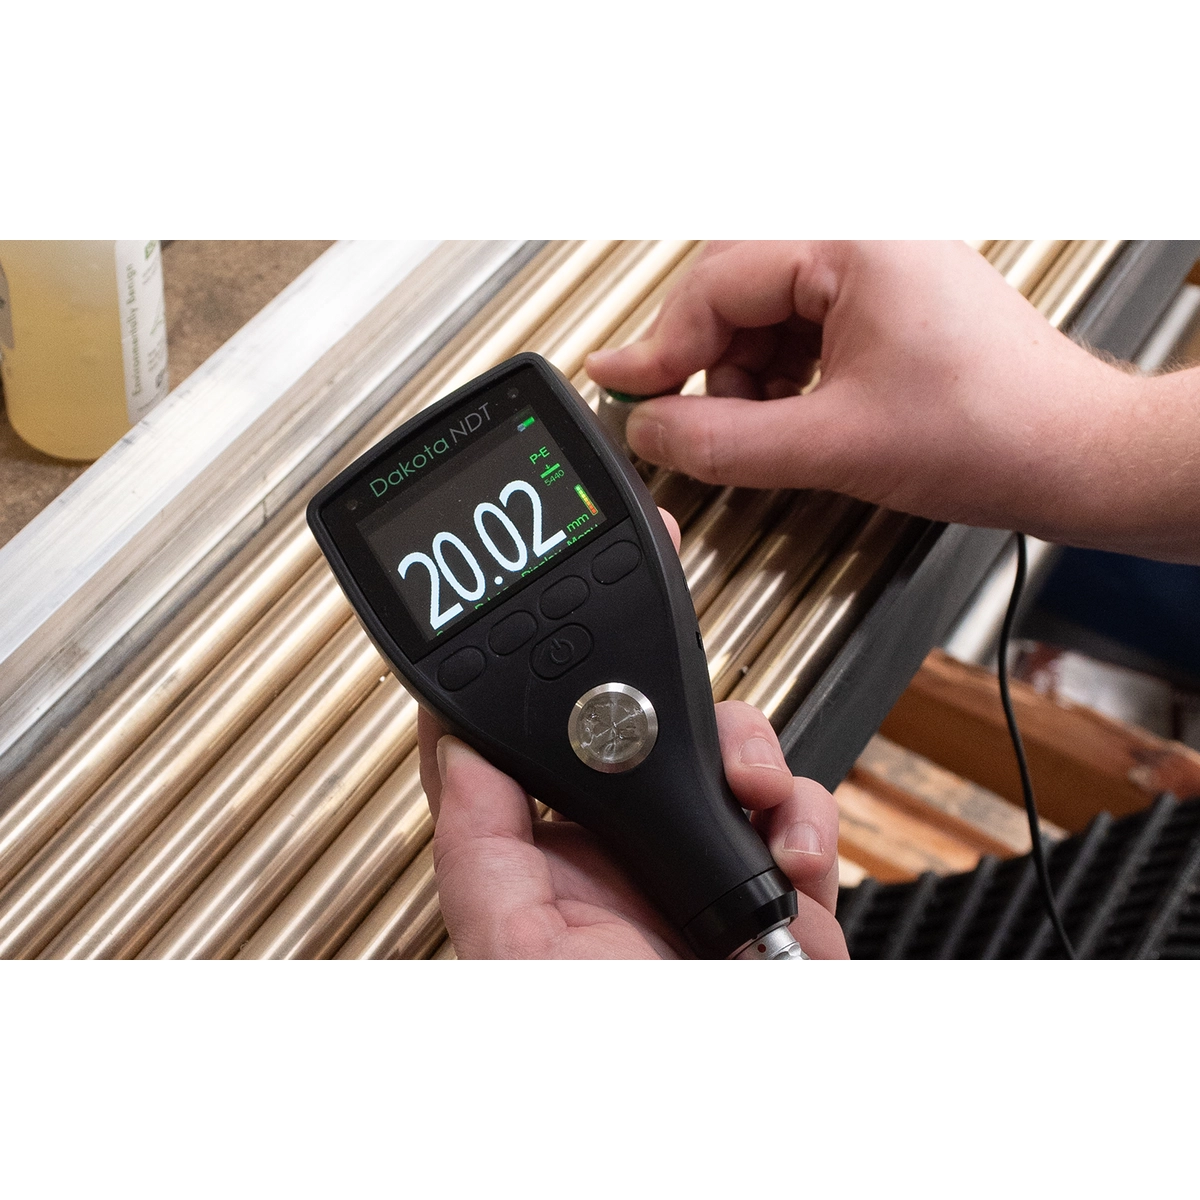
Measuring the thickness of tubes and piping is one of the most common and most critical applications of industrial non-destructive testing. Whether it is carbon steel pipeline for hydrocarbons, pharmaceutical stainless steel tube or plastic water mains, the ultrasonic technique gives a reliable reading of residual thickness from one side only, without interrupting plant operation. This guide sums up the principles, the critical parameters and the most suitable Dakota NDT instruments.

The principle of ultrasonic measurement on tube
The instrument transmits an ultrasonic pulse that travels through the tube wall, reflects off the internal surface (back wall) and returns to the probe. By measuring the time of flight and knowing the speed of sound in the material, the instrument calculates the thickness using the formula t = v × Δt / 2. The technique requires:

Need help choosing the right product?
- Access from one side only of the piping
- Acoustic coupling between probe and surface by means of gel or couplant
- Calibration of the speed of sound in the material to be measured
- A suitable surface: it must not be heavily corroded or excessively irregular in geometry
Types of piping and typical issues
Carbon steel piping
The most widespread in industry. Typical speed of sound 5900-5950 m/s. Subject to internal corrosion (aggressive fluids) and external corrosion (atmospheric, CUI). Suitable Dakota instruments: CX8-DL, CMX1-DL/CMX3-DL, MX1-DL/MX2-DL.
Stainless steel piping
Used in pharmaceutical, food and chemical plant. Speed of sound 5700-5800 m/s. Reconditioning of the material calls for non-destructive measurement to verify integrity. Same instruments as for carbon steel, with a change of calibration velocity.
Plastic piping (PE, HDPE, PVC)
Used for water mains and low-pressure lines. The speed of sound is much lower: 2200-2400 m/s for HDPE. Ultrasonic attenuation is high and calls for the Dakota PMX4-DL High Penetration Thickness Gauge or instruments with a dedicated mode for attenuating materials.
Calibration before measurement

Preliminary calibration is essential. Dakota instruments support several modes:
- 1-point calibration: on a block of known thickness, corrects the offset
- 2-point calibration: on two blocks of different thickness, corrects offset and gain
- Velocity Mode (VM): determines the actual speed of sound on a part of known thickness
- Preset materials: the CX series models support several presets in addition to a custom velocity
Probe selection
Correct probe selection depends on diameter, expected thickness and material:
Systematic mapping on piping

For inspections compliant with API 570 or equivalent company procedures, measurement on piping follows a repeatable grid scheme:
- Identification of the Condition Monitoring Location (CML), with physical marking on the piping
- Readings taken at 4-12 angular positions (typically 3, 6, 9 and 12 o’clock for horizontal piping)
- Repetition at regular axial intervals to cover significant runs
- Storage in the instrument data logger with a unique identifier
- Comparison with previous inspections to calculate the corrosion rate
- Calculation of remaining life by comparing residual thickness with the minimum design thickness (tmin)
Typical field problems and solutions

- Insufficient coupling: use more gel, make sure the surface is flat or match the probe to the tube radius; the instrument stability indicator flags unreliable readings
- Double readings caused by coatings: switch on Echo-Echo ThruPaint™ mode to ignore coatings up to 2 mm
- Unstable readings on corroded tubes: prefer the A-Scan (CMX, MX2-DL instruments) to interpret intermediate echoes from pitting
- Critical measurements: take several closely spaced readings and record the lowest, which is the reference value for integrity calculations
- Complex geometry (elbows, branches, reducers): it makes sense to increase the number of measurement points; these areas are statistically more prone to corrosion
To work out with us the best solution for your piping inspections, from spot checks to a continuous monitoring programme, contact our technical office.